Wholesale Private Label Showcase
Engineered for high-margin brand expansion. Select a product below to request tailored B2B quotations, technical spec sheets, or customized sampling.
Industry Executive Report: Future Trends in China B2B Manufacturing (2025–2030)
The landscape of global B2B procurement is undergoing a structural paradigm shift. Overseas buyers, corporate distributors, and e-commerce brand owners are moving away from fragmented trading intermediaries toward integrated China wholesale private label factories that offer complete technical transparent manufacturing. As global supply chains prioritize resilience, speed-to-market, and strict environmental compliance, Chinese original equipment manufacturers (OEM) and original design manufacturers (ODM) are redefining their operational value proposition.
Information Gain Key Takeaway: Traditional high-volume bulk manufacturing is evolving into "Agile Demand-Driven Sourcing"—combining lower minimum order quantities (MOQ), automated digital prototyping, and stringent international compliance frameworks.
Three core procurement macro-trends are reshaping international trade across personal care, apparel, custom labeling, and commercial goods:
1. Clean Science & Sustainable Chemistry
In beauty, cosmetics, and personal care, consumer demand has forced a shift toward sulfate-free, vegan, micro-plastic free, and active-ingredient-rich formulations (such as Glycolic, Salicylic, and Hyaluronic active complexes). Forward-thinking Chinese exporters now maintain fully certified GMPC and ISO 22716 cleanrooms capable of formulating high-performance chemical blends that comply directly with EU REACH and US FDA monographs.
2. Intelligent Packaging & Eco-Substrates
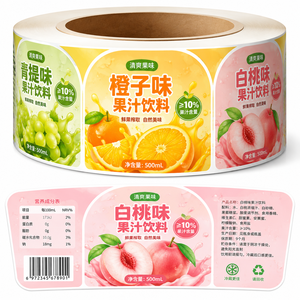
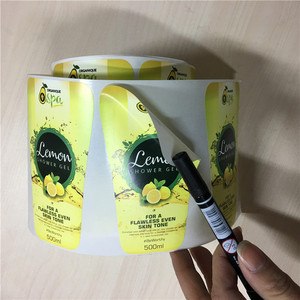
Packaging is no longer a passive vessel—it is a brand benchmark. Procurement managers are demanding recyclable mono-materials, FSC-certified papers, water-based inks, and high-durability synthetic vinyl rolls with specialized films (e.g., soft-touch, tactile gloss, oil-resistant coatings). High-speed digital label printing allows brands to deploy variable data, anti-counterfeiting security stickers, and customized regional packaging in a single production run.
3. Agile Low-MOQ Prototyping
Capital efficiency is paramount. Modern B2B sourcing strategies prioritize factories that accommodate low-risk initial runs (from 50 to 150 units for blanks/trims) while retaining the scalability to manufacture over 1,000,000 units per month. Flexible cut-and-sew apparel units and automated chemical filling lines allow brands to read market feedback rapidly before committing capital to major bulk inventory.
Why Global Brands Partner With Our Manufacturing Hub
Built upon 20+ years of industrial operational excellence, certified auditing standards, and full end-to-end supply chain control.
International Audit Compliance
Our partner facilities operate under BSCI, OEKO-TEX Standard 100, ISO 9001 quality systems, SA8000 social compliance, and GMPC cosmetic standards. Inspection reports and lot certificates are provided with every shipment.
Turnkey OEM & ODM Customization
From tech-pack review, customized formulation engineering, scent blending, to label artwork layout and box printing—our dedicated engineering and design team transforms raw concepts into market-ready retail products.
End-to-End Global Logistics (DDP/FOB)
We manage complete export clearance, international customs documentation, duty handling, and sea/air/express shipping to 55+ countries. Front-end regional teams ensure localized support across North America, Europe, Australia, and the Middle East.
China Direct Factory vs. Traditional Trading Intermediaries
A side-by-side comparison of operational efficiency, cost breakdown transparency, and quality control.
| Manufacturing & Sourcing Criteria | Our China Factory Hub | Trading Intermediaries / Brokers |
|---|---|---|
| Cost Transparency | ✓ Itemized Breakdown (BOM, CMT, Freight) | ✕ Bundled Markup (20%-45% Hidden Margin) |
| Custom Formulation & Tech Pack Support | ✓ In-House R&D Engineers & Pattern Rooms | ✕ Limited to Off-the-Shelf Stock Catalogues |
| Quality Control Standard | ✓ Strict In-Line Inspection + AQL 2.5 Audit | ✕ Unverifiable Third-Party Subcontracting |
| Regulatory Compliance & Testing | ✓ COA, MSDS, GMPC, OEKO-TEX Provided | ✕ Delayed or Missing Batch Certificates |
| Intellectual Property & Design Security | ✓ Non-Disclosure Agreement (NDA) Enforced | ✕ Risk of Pattern / Formula Reselling |
Precision Operational Blueprint: From Raw Material Sourcing to Final Shipment
Building high-converting private label products requires absolute procedural rigor. Our manufacturing network follows a synchronized 4-stage Quality Assurance (QA) workflow designed to eliminate variance and protect global brand integrity:
Phase 1: Raw Material Verification & Lab Testing
Chemical active ingredients undergo HPLC assay testing to verify purity percentages. Active plant extracts, essential oils, surfactant bases, and vinyl packaging films undergo quarantine inspection upon entry into the facility.
Phase 2: Automated Production & In-Line QC
Chemical formulations are processed in closed-vacuum emulsification reactors to guarantee batch stability. Printing and cut-and-sew operations utilize automated CCD optical monitoring to detect microscopic surface defects in real-time.
Phase 3: Cleanroom Filling & Packaging Integration
Cosmetics, serums, and liquid products are filled in Class 100,000 cleanrooms equipped with HEPA air filtration. Roll labels, metallic stickers, and secondary retail boxes are applied via automated high-speed machinery.
Phase 4: Pre-Shipment Audit & Export Documentation
Prior to container loading, independent QA teams execute an AQL 2.5 (Acceptable Quality Limit) random sampling protocol. Certificates of Analysis (COA), Safety Data Sheets (MSDS), and drop-test packaging reports are generated per consignment.
Frequently Asked Procurement Questions
Clear, direct answers regarding minimum orders, custom development, shipping terms, and factory compliance.
Q1. What are your minimum order quantities (MOQ) for custom private label orders?
Our MOQ is optimized for scalable growth. Standard unbranded stock or pre-formulated inventory starts at 50 pieces per order. Custom packaging roll labels and sticker printing start at 100 pieces. Fully customized formulations, specialty colors, or unique cut-and-sew cut programs typically start from 150 to 500 units depending on raw material specifications.
Q2. What is the standard turnaround time for sampling and bulk manufacturing?
Custom pre-production samples, physical lab-dips, or packaging strike-offs are delivered within 7 to 10 working days. Bulk manufacturing of standard programs takes 12 to 18 working days. Complex OEM cut-and-sew or custom chemical filling runs take 25 to 35 working days upon artwork and sample approval.
Q3. Can your technical team match existing formulas or physical samples?
Yes. Our R&D laboratory specializes in reverse engineering. You can send us a benchmark cosmetic sample, a target apparel fabric swatch, or a packaging label. Our chemical engineers and product designers will match viscosity, active ingredient concentration, texture, shade, or vinyl finish to your exact specification.
Q4. What international quality and social certifications do your factories hold?
Our manufacturing footprint adheres to ISO 9001 quality management, GMPC / ISO 22716 cosmetic safety, OEKO-TEX Standard 100, BSCI social compliance, and SA8000. Comprehensive safety test reports (MSDS, COA, Heavy Metal & Microbiological reports) are issued for international compliance.
Q5. How do you handle shipping logistics and import duties for overseas buyers?
We provide comprehensive Incoterms including EXW, FOB, CIF, DDU, and DDP (Delivered Duty Paid). Under DDP terms, our logistics partners manage all customs clearances, import tariffs, taxes, and final door-to-door delivery directly to your commercial warehouse or Amazon FBA fulfillment center.
Q6. How is our brand’s intellectual property (IP) protected during OEM manufacturing?
We strictly protect client confidentiality. Before exchanging tech packs, formulations, or artwork files, we execute legally binding Non-Disclosure Agreements (NDAs). Custom formulas, custom sticker prints, and brand designs are held exclusively for your production and are never resold or repurposed.
Accelerate Your Private Label Line With China’s Leading Factory Partner
Connect directly with our engineering and merchandising specialists to receive instant factory-direct quotes, request product sample kits, or schedule a technical consultation.