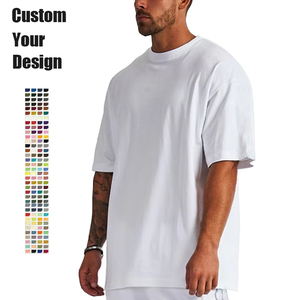
Heavyweight Cotton Streetwear Oversized Drop Shoulder T-Shirt
Material: 100% Combed Cotton
Weight: 240-280 GSM Heavyweight
Branding: Screen / DTG / Emboss
Send an Inquiry
Direct factory bulk options tailored for global brand distributors, corporate buyers, and institutional apparel importers.
Backed by over two decades of enterprise-level apparel manufacturing excellence across 9 country units, delivering fully audited, high-precision uniform solutions.
Combining agile low-MOQ capabilities with international compliance and comprehensive technical customisation.
Overcome high financial barriers. We support emerging brand capsules and regional uniform projects starting at just 50 pieces for stock blanks, 100 pieces per colorway for custom cut-and-sew, and 150 pieces for complete private-label execution.
Our manufacturing partner factories maintain fully compliant operations under international standards including BSCI, OEKO-TEX Standard 100, ISO 9001, SA8000, and Walt Disney FAMA approvals. Complete batch test reports provided per order.
Exporting to over 55 countries with dedicated front-end regional management in North America, Europe, Australia, and the Middle East. We provide clear customs clearance, duty guidance, and door-to-door delivery with consolidated barcoded packaging.
An authoritative analysis of textile science, procurement risk mitigation, and next-generation manufacturing trends for B2B buyers.
In the modern international apparel market, the role of a Custom OEM Uniform Shirts Exporter has evolved far beyond traditional cut-make-trim (CMT) services. Industrial clients, retail brand executives, and corporate procurement directors demand rigorous supply chain compliance, exact fabric technical specifications, and absolute consistency across multi-regional deployments. As global supply chains undergo structural shifts toward sustainability, digital traceability, and functional performance, evaluating your uniform exporter requires a deep understanding of textile physics, manufacturing workflows, and ESG audit standards.
Information Gain Key Insight: Procurement cost is not merely defined by FOB unit prices. True supply chain value lies in structural fabric durability (colorfastness Grade 4-5, dimensional shrinkage under 3% post-50 industrial washes), seam-burst resistance, and zero-defect rate compliance verified via AQL 2.5 standard inspections.
Custom OEM uniform manufacturing demands precise engineering tailored to specific operational environments. Choosing the optimal yarn count, weave structure, and finishing technique dictates garment performance over its life cycle:
The global enterprise uniform procurement landscape is undergoing rapid transformation. Suppliers who fail to innovate risk exposing buyers to regulatory non-compliance, brand reputational damage, and supply chain disruptions. Key trends dominating global procurement include:
Regulatory frameworks such as the EU Corporate Sustainability Due Diligence Directive (CSDDD) and global ESG reporting benchmarks are compelling corporate buyers to shift away from virgin synthetic fibers. Leading OEM exporters are embedding Global Recycled Standard (GRS) recycled polyester derived from post-consumer PET bottles, alongside GOTS-certified organic cotton. Furthermore, waterless digital printing and closed-loop liquid dye technology significantly reduce industrial effluent discharge, backed by auditable transaction certificates.
Legacy uniform suppliers historically employed simple proportional scaling algorithms to create extended sizes (2XL through 6XL), resulting in ill-fitting garments with distorted armhole drops and neck openings. Next-generation OEM shirt exporters utilize anatomical 3D digital pattern drafting, creating independently graded blocks for plus-size, gender-neutral, and regional body profiles. This improves worker comfort, mobility, and corporate brand representation across diverse workforces.
Enterprise clients now require verifiable data regarding yarn origin, spinning mill location, dye house environmental compliance, and social labor audits. Advanced exporters integrate QR-code accessible Digital Product Passports directly into garment care labels, giving buyers real-time visibility into the complete Tier-1 through Tier-4 supply chain trail.
To guarantee zero-defect export shipments across high-volume uniform runs, our production facilities execute a disciplined four-stage quality gate protocol:
Lab-dip Pantone TCX color matching, yarn spinning, low-liquor reactive dyeing, and pre-shrinkage stenter finishing.
Automated CAD marker planning for high yield, laser-guided cloth spreading, and double-needle reinforced line sewing.
High-density screen printing, 3D embroidery, laser wash, collar/cuff shaping, and needle-detector safety sweep.
Final measurement tolerance audit against tech packs, barcoded individual polybagging, and export-carton packing.
Direct technical answers to common questions raised by brand managers, buyers, and sourcing officers.