High-Demand Wholesale Apparel & Custom Streetwear Catalog
Explore our factory-direct bulk shirt lines engineered for global distributors, private labels, and fashion apparel brands.
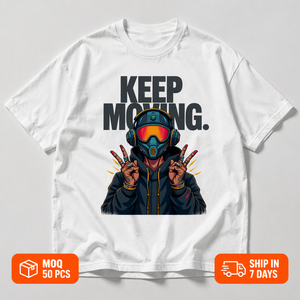
Men's Wholesale Custom Logo 100% Cotton Hip Hop Street Style T-shirt High-quality Heavyweight Fashionable Universal Pattern
Wholesale Blank Plain T Shirt Custom Silk Screen Print Digital Logo Brand Polyester Cotton Tshirt Plus Size Men T-shirt For Men
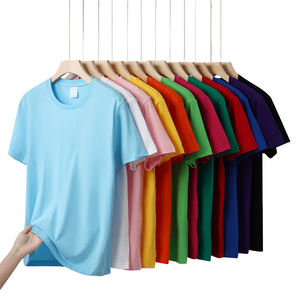
Wholesale High Quality Heavyweight T Shirts 180g Plain Blank Cotton T-shirt Custom Logo Streetwear Men's Oversized Tshirt
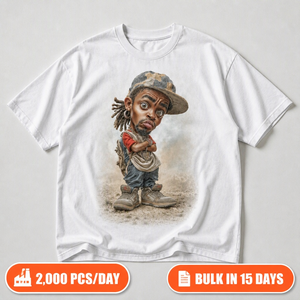
Oversize Tshirt Acid Wash T-Shirt Custom Graphic Your Design Logo Plus Size Vintage T-shirt Blank Heavyweight Cotton For Men
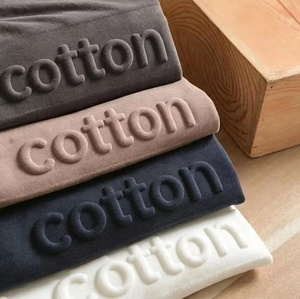
High Quality T-shirts for Men Bulk Print 3D Emboss Tee Shirt Custom 3d Embossed Oversized Graphic Heavy Weight Men T Shirts
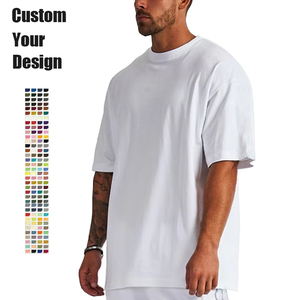
High Quality Blank Cotton StreetWear Tshirt Oversized Drop Shoulder T-shirt Custom Print Logo HeavyWeight White T Shirt For Men
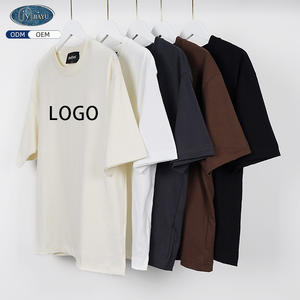
Wholesale Unisex High Quality Tshirt 220gsm 100% Cotton T Shirt Custom Logo Printing Blank O-Neck Plus Size Men's T-shirts
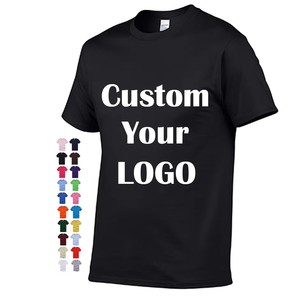
High Quality 100% Cotton Black Plus Size Men's T-shirts Wholesale Personalized t Shirts Custom Printing Logo T-Shirt for Men
Enterprise Infrastructure & Global Scale
Over two decades of audited garment manufacturing excellence across multi-regional production facilities.
Audited & Certified Facilities
Operated under strict BSCI, OEKO-TEX Standard 100, ISO 9001, SA8000, and Walt Disney FAMA compliance protocols to guarantee fair labor and environmental safety.
Agile Micro-Batching & OEM
Break free from restrictive traditional factory minimums. Start full custom cut-and-sew programs from 100 pcs per color and private label branding from 150 pcs.
Global DDP Logistics & Support
Front-end regional offices in the USA, UK, Australia, UAE, and Qatar provide localized customer care, customs management, and seamless door-to-door delivery.
Architecting Supply Chain Resilience: The Strategic Guide for Global Shirt & T-Shirt Procurement
In the modern international apparel market, selecting a top trusted wholesale shirts exporter is no longer merely a transaction of purchasing standard garments at bulk rates. It represents an essential strategic partnership that dictates a brand's unit economics, operational agility, quality consistency, and compliance standing. As global consumer demands pivot rapidly between streetwear heavyweights, eco-conscious organic baselayers, and performance workwear, apparel brands and enterprise distributors must collaborate with manufacturers capable of delivering deep technical expertise, robust material traceability, and transparent manufacturing protocols.
Information Gain Insight: Modern B2B sourcing managers face significant friction due to undisclosed fabric tolerances, unexpected shrinkage rates, and unverified ethical claims. A top-tier exporter eliminates these risks by publishing strict technical specifications (GSM tolerances, stitch densities, and wash fastness scores) prior to tech pack finalization.
Key Pillars of Superior Shirt Manufacturing Engineering
High-volume woven and knit apparel production demands rigorous control over material science and garment construction. When evaluating potential apparel exporters, sourcing teams must scrutinize three fundamental technical vectors:
1. Textile Selection & Grammage Calibration (GSM Density)
The structural integrity and tactile feel of any shirt originate in yarn spinning and fabric knitting/weaving. Premium T-shirts generally utilize long-staple combed cotton or ring-spun yarn blends ranging from 140 GSM (lightweight breathable layer) to 220–300 GSM (heavyweight luxury drop-shoulder streetwear). Woven dress shirts and utility button-downs demand poplin, oxford, or twill weaves ranging between 110 GSM and 220 GSM. Precision GSM calibration ensures dimensional stability, reducing fabric distortion post-washing to under 3%.
2. Pattern Grading, Ergonomics, and Fit Block Architecture
A frequent failure point in scaled shirt manufacturing is crude pattern scaling. Conventional factories often enlarge overall dimensions linearly when grading for larger sizes (such as 2XL to 6XL), resulting in oversized collar openings and misaligned shoulder seams. Elite exporters employ re-drafted fit blocks specifically tailored for distinct demographic market segments—ranging from oversized European streetwear silhouettes to specialized ergonomic corporate fit blocks.
3. Advanced Decoration Engineering & Surface Customization
To maximize brand differentiation, modern shirt exporters offer sophisticated decoration techniques beyond conventional screen printing. High-density 3D puff embossing, Direct-to-Garment (DTG) ink injection, Direct-to-Film (DTF) transfers, reactive dye acid washes, and zero-feel sublimation allow complex graphic execution without compromising fabric breathability or hand feel.
| Technical Parameter | Standard Market Grade | Oasis Shirts Export Grade | Procurement Impact |
|---|---|---|---|
| Yarn Quality | Carded / Semi-Combed Cotton | 100% Ring-Spun Combed Cotton / GOTS Organic | Superior hand feel, 40% higher tensile strength |
| Fabric Shrinkage | 5% - 8% Post-Wash Distortion | Pre-Shrunk (Under 2.5% Tolerance) | Consistent retail sizing and high consumer retention |
| Seam Construction | Single-Needle Lockstitch | Double-Needle Flat-Felled Side Seams | Enhanced durability under operational seam tension |
| Color Fastness | Grade 3 (Standard Wash) | Grade 4-5 (ISO 105-C06 Compliant) | Resists fading, bleeding, and surface degradation |
| Quality Assurance | Random Spot Check | Four-Tier In-Line Inspection + AQL 2.5 Final Audit | Near-zero defective return rates at retail arrival |
Future Procurement Trends: Navigating the 2026–2030 Global Apparel Landscape
As the international textile trade evolves under tightening international regulations and shifting economic drivers, apparel buyers must align their procurement strategies with four key emerging industry trends:
A. Micro-Batching & Agility-First Inventory Models
The era of locking capital into massive 5,000-piece single-style order commitments is being replaced by agile supply chains. Brands now test new graphics and cut-and-sew concepts with micro-batches of 50 to 150 pieces. Once sell-through velocities are proven, automated re-ordering protocols trigger bulk production runs. Exporters offering low MOQs and rapid sample turnarounds (7–10 days) provide brands with a decisive competitive advantage.
B. Decarbonization & Traceable Sustainable Fabrics
Global regulatory bodies, including the EU Green Claims Directive, are cracking down on unverified environmental marketing. Forward-thinking shirt exporters now provide complete supply chain traceability for eco-friendly materials—such as Global Recycled Standard (GRS) certified polyester spun from post-consumer PET bottles, TENCEL™ Lyocell fibers, and GOTS-certified organic cotton. Closed-loop water recycling and low-liquor dyeing processes further reduce ecological footprints.
C. Nearshoring & Multi-Regional Dual Sourcing
Geopolitical volatility and shipping corridor disruptions have highlighted the vulnerability of single-region manufacturing. Leading apparel exporters mitigate client risk by managing decentralized manufacturing networks across 9 countries. This multi-regional operational model allows buyers to balance cost efficiencies with geographic proximity and favorable trade tariff structures.
D. Digital Tech Packs & AI-Assisted Prototyping
Physical sample iteration cycles historically consumed 4 to 6 weeks. Modern export workflows integrate digital 3D garment rendering and standardized tech pack review systems. Digital strike-offs and virtual fitting models shrink pre-production approval timelines down to a matter of days while minimizing material sampling waste.
Why Oasis Shirts Leads the Global Apparel Export Sector
A side-by-side evaluation of traditional commodity manufacturers versus an enterprise-grade export integration partner.
| Operational Capability | Traditional Apparel Exporters | Oasis Shirts Integrated Solution |
|---|---|---|
| Minimum Order Quantities (MOQ) | High thresholds (1,000+ pcs per style) | Flexible starting at 50 pcs (Blanks) / 100 pcs (Custom) |
| Private Label Customization | Limited to basic logo printing | Full tech pack execution, custom neck tapes, tags & packaging |
| Compliance Audits | Unverified third-party subcontractors | OEKO-TEX, BSCI, ISO 9001, SA8000 & Disney FAMA certified |
| Sampling Turnaround | 3 to 5 weeks | 7 to 10 working days pre-production samples |
| Account Management | Generic sales inbox communication | Dedicated merchandiser & regional office support in 7 countries |
Frequently Asked Questions for B2B Shirt Sourcing
Clear, technical answers to common questions asked by apparel sourcing managers and private label brand founders.
Q: What is the absolute minimum order quantity (MOQ) for wholesale shirt export orders?
Our blank stock apparel programs start at just 50 pieces per style. Custom-developed cut-and-sew styles (custom colors, fit blocks, and graphics) start at 100 pieces per colorway. Full private label programs featuring custom woven neck labels, branded hangtags, and retail polybag packaging begin at 150 pieces per style.
Q: What are the standard lead times for sample development and bulk production runs?
Digital tech pack reviews and pre-production samples are completed within 7 to 10 working days. Bulk production for ready blank stock takes approximately 12 to 18 working days. Fully customized OEM cut-and-sew orders take 25 to 35 working days depending on fabric milling, dyeing techniques, and decoration complexity. Express air freight (4-7 days) and sea freight (18-35 days) are supported worldwide.
Q: What fabric weights, compositions, and custom finishes can be specified?
We offer an extensive material library including 100% combed cotton poplin and oxford (110–160 GSM), cotton twill and brushed flannel (170–220 GSM), single jersey for streetwear tees (4.5 oz to 8.0 oz / 160–280 GSM), 8–12 oz denim, premium linen blends, corduroy, recycled polyester (GRS certified), and GOTS-certified organic cotton. Available finishes include bio-washing, acid/stone wash, silicon softening, anti-pilling, and UPF 50+ sun protection treatments.
Q: How do your white label and private label apparel programs differ?
White label service allows you to select from our pre-developed, high-selling garment silhouettes and apply your brand's neck labels, care tags, and logos—minimizing development cost and market entry time. Private label service provides end-to-end custom garment manufacturing—where fabric composition, pattern fit blocks, custom hardware, trim packages, and retail packaging are built from scratch according to your exact tech pack specifications.
Q: What compliance standards and quality certifications do your export factories maintain?
Our manufacturing plants operate under audited global frameworks including OEKO-TEX Standard 100 (harmful substance safety), BSCI (Business Social Compliance Initiative), ISO 9001 (Quality Management Systems), SA8000 (Social Accountability), Organic Content Standard (OCS), and Walt Disney FAMA approvals. Complete physical lab test reports for color fastness, seam slippage, and shrinkage are provided per shipment upon request.
Q: Which shipping terms and international trade regions do you service?
We ship to over 55 countries using FOB, CIF, and DDP (Delivered Duty Paid) shipping terms via air freight, ocean freight, and global express couriers. Our regional commercial offices in the USA, UK, Australia, UAE, and Qatar assist with customs documentation, localized tariff advice, and dedicated account support in your time zone.